Occidental Petroleum Approved Heat Exchanger Suppliers: What the Standard Really Requires
When a heat exchanger is destined for a project linked to Occidental Petroleum, the American oil and gas company headquartered in Houston, Texas, "approved supplier" is not a phrase any manufacturer can adopt on its own. It is a specific, audited status that Occidental Petroleum grants to individual manufacturers after a formal qualification process. For procurement and engineering teams in Dubai and across the GCC researching Occidental Petroleum Approved Heat Exchanger Suppliers, understanding what that process actually involves is far more useful than searching for a badge or a claim on a website.
This article explains what Occidental Petroleum vendor approval covers for heat exchangers, the engineering baseline it is built on, and what to check for when qualifying a manufacturer for Occidental-linked or Occidental-grade heat exchanger projects.
What Vendor Approval Actually Means
Occidental Petroleum maintains its own vendor qualification requirements, and getting listed involves a detailed audit of a manufacturer's quality management system, tube bundle fabrication capability, welding practices, non-destructive testing capability, and documented fabrication history for shell-and-tube and other heat transfer equipment used across its upstream, chemical, and enhanced oil recovery operations. That audit is typically carried out by Occidental's own inspection personnel or by a third-party inspection agency acting on its behalf. The resulting approval is specific to the manufacturer and often to defined exchanger categories, design codes, and product classes.
Because this status is granted directly by Occidental Petroleum to a named manufacturer, it is not something any supplier can claim without going through that process. What buyers researching suppliers can assess independently, before any formal audit, is whether a manufacturer's engineering and quality practices are already built to the level Occidental-grade heat exchanger work requires.
How the Audit Process Works
The audit typically begins with a document review of the manufacturer's quality manual, tube-to-tubesheet welding procedures, and past exchanger delivery records, followed by an on-site facility inspection covering shell fabrication, tube bundle assembly, tubesheet welding, and testing procedures such as shell-side and tube-side hydrostatic testing.
What Approval Is Tied To
Approval is rarely a blanket status. It is usually specific to exchanger type (fixed tubesheet, U-tube, or floating head), design code, TEMA class, and the product classes the manufacturer has demonstrated competence in during the audit.
Why Occidental-Grade Heat Exchangers Carry Their Own Qualification Demands
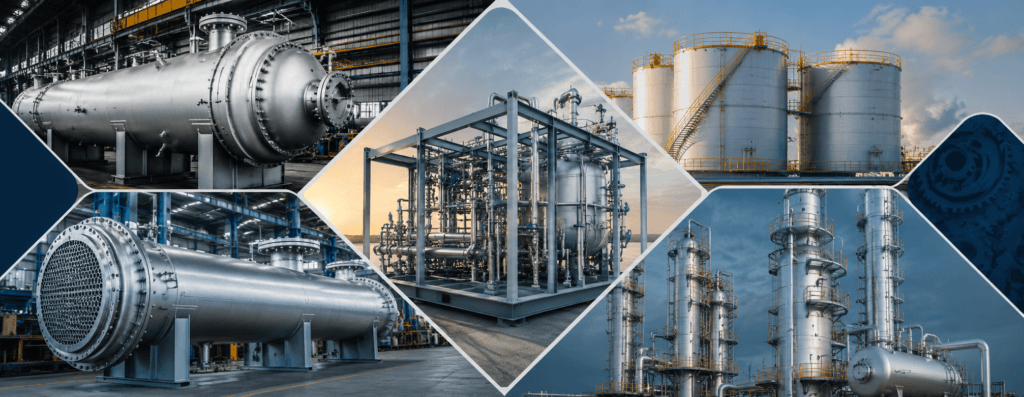
Heat exchangers used across Occidental's upstream and chemical processing facilities transfer thermal energy between process streams under demanding pressure and temperature conditions, where a tube-to-tubesheet weld defect, baffle misalignment, or shell fabrication error can lead to cross-contamination, reduced thermal performance, or a serious safety incident. Unlike simpler shop-fabricated equipment, Occidental-grade exchangers involve precision tube bundle fabrication, tubesheet integration, and full pressure testing on both shell and tube sides, all of which must be controlled to a consistent standard from design through final inspection and handover.
That is why exchanger qualification for Occidental-linked work places heavy weight on tube-to-tubesheet joint integrity, baffle spacing accuracy, and full dual-side hydrostatic testing before dispatch, rather than only checking the finished shell. A supplier being evaluated for this level of work needs to demonstrate control over the full build sequence: tube bundle design, tubesheet and shell integration, welding, and final testing and inspection, all traceable under one consistent quality system. This is the same discipline that governs related equipment such as pressure vessels, columns, and reactors, where integrity under demanding upstream and chemical process conditions is equally non-negotiable.
Product Containment and Site Delivery Considerations
Occidental-linked heat exchangers are frequently fully assembled and factory-tested before being shipped as complete transportable units to upstream and chemical processing facilities, where transport dimensions, lifting point design, and site tie-in points matter as much as the exchanger's thermal duty, particularly given the limited scope for correction once a tube bundle has been fabricated, tested, and dispatched. Exchangers commonly integrate removable bundles and floating heads to simplify future maintenance and re-tubing.
Consequences of Fabrication Defects
An undetected tube-to-tubesheet weld defect or baffle misalignment can surface only after commissioning as a pressure test failure, a cross-contamination event, or an unplanned shutdown, making thorough dual-side hydrostatic testing far more valuable than post-installation repair on a live exchanger within an operating facility.
The Engineering Baseline Behind Occidental-Grade Heat Exchangers
Regardless of an exchanger's final destination, the technical requirements underpinning Occidental-grade fabrication are largely the same requirements that govern quality heat exchanger manufacturing generally:
Design Code — TEMA standards for mechanical design, combined with ASME Section VIII for the pressure-retaining shell and tubesheet, and ASME B31.3 for connected piping.
Material Traceability — Full mill test certificates and heat-number traceability for shell plates, tubes, tubesheets, and baffle components.
Welding Procedure Qualification — WPS and PQR documentation, with welders individually qualified under ASME Section IX for shell, tubesheet, and tube-to-tubesheet welds.
Non-Destructive Testing — Radiographic or ultrasonic examination of shell welds, dye penetrant testing of tube-to-tubesheet joints, and visual inspection of all fabricated joints.
Dimensional and Structural Verification — Tube pitch, baffle spacing, and shell diameter checked against approved general arrangement and thermal design drawings before closeout.
Design Review and Calculations — Thermal duty calculations, shell and tubesheet thickness, and support loading reviewed against the specified process and utility conditions.
Factory and Site Acceptance Testing — Shell-side and tube-side hydrostatic pressure testing, and tube expansion verification, confirming integrity before the exchanger is placed into service.
Third-Party Inspection — Hold-point sign-off from an accredited inspection body such as Lloyd's Register, Bureau Veritas, TÜV, or DNV at critical stages of fabrication and testing.
A manufacturer that applies this level of control as standard practice, not only on projects with a named end client, is generally the one positioned to succeed if and when a formal Occidental-linked audit takes place.
Where Nordstone Fits
Nordstone designs and manufactures process equipment for the Oil & Gas, Petrochemical, Energy, and Water Treatment sectors, serving Dubai, the wider UAE, GCC, and international markets, with more than 20 years of combined engineering experience across the team. Our fabrication and QA/QC processes are structured around the technical baseline described above: documented material traceability, ASME IX-qualified welding, tube bundle and tubesheet integration control, comprehensive NDT, and full dual-side pressure testing before handover.
To be clear with buyers researching this topic: formal vendor approval with Occidental Petroleum is issued directly by Occidental to specific manufacturers following its own audit process, and we are not claiming that status here. What we can speak to with confidence is the engineering rigor our heat exchangers are built to on every project.
Equipment Built to That Standard
Heat Exchangers — TEMA-designed shell-and-tube units for heating, cooling, condensation, and energy recovery.
Pressure Vessels — ASME Section VIII-compliant vessels engineered for safe containment under demanding pressure and temperature conditions.
Columns — Distillation, absorption, and stripping columns engineered for process efficiency in refining and petrochemical service.
Reactors — Process reactors engineered for controlled chemical reactions under demanding operating conditions.
Process Skids — Factory-assembled modular skids integrating vessels, pumps, piping, and instrumentation.
Storage Tanks — API 650/620-referenced tanks for liquids, gases, chemicals, and petroleum products.
Frequently Asked Questions (FAQs)
1. What does "Occidental approved" mean for a heat exchanger supplier? It means Occidental Petroleum has directly qualified the manufacturer, auditing plant capability, welding, material control, testing procedures, and code compliance specific to its own contracts. It is a formal, client-issued status, not something a manufacturer can claim on its own.
2. How does a heat exchanger manufacturer get onto Occidental's approved list? Occidental reviews the manufacturer's QA/QC systems, code compliance (TEMA and ASME Section VIII), material traceability, welding procedure qualifications, testing practices, and inspection records, typically followed by a facility audit.
3. Is Nordstone an Occidental-approved heat exchanger supplier? Nordstone is not claiming formal Occidental-approved status. What we can speak to is our own engineering baseline: code-compliant design, full material traceability, certified welding procedures, tube bundle and tubesheet integration control, and third-party NDT and pressure testing documentation, the same baseline vendors need before approval is even considered.
4. What should buyers verify before shortlisting a heat exchanger supplier for Occidental-linked projects? Check for current TEMA and ASME Section VIII code compliance, welder and procedure qualifications, material and weld traceability records, dual-side hydrostatic testing documentation, references from upstream or chemical processing projects, and clarity on approval status versus working toward it.
5. What standards should heat exchanger fabrication follow regardless of approval status? TEMA standards for mechanical design combined with ASME Section VIII for the pressure-retaining shell and tubesheet, with full documentation for materials, welding, tube bundle assembly, and dual-side pressure testing, the groundwork any approval process builds on.
Working With Nordstone
If your project requires heat exchangers engineered to international codes and manufactured under documented quality control, our engineering team can review your thermal duty, capacity, and site requirements and provide a project-specific proposal. Get in touch with Nordstone to discuss your specifications.
Get In Touch
Recent Posts